
Aluminum alloy is suitable for certain non-pressure-bearing structural parts in oil and gas equipment, such as instrument housings, mounting panels, support brackets, and auxiliary structural components. Its low density and good machinability make it suitable for applications where weight and dimensional accuracy need to be balanced. For equipment exposed to moisture, salt, and corrosive media, the machining plan should also consider the material grade, part structure, and operating conditions to ensure that lightweight design remains compatible with the actual application environment.
Which Oil & Gas Equipment Aluminum Alloy Parts Are Suitable for CNC Machining?
Aluminum alloy is more suitable for non-pressure-bearing structures that have been confirmed through engineering design, while the function of each part determines the specific machining requirements.
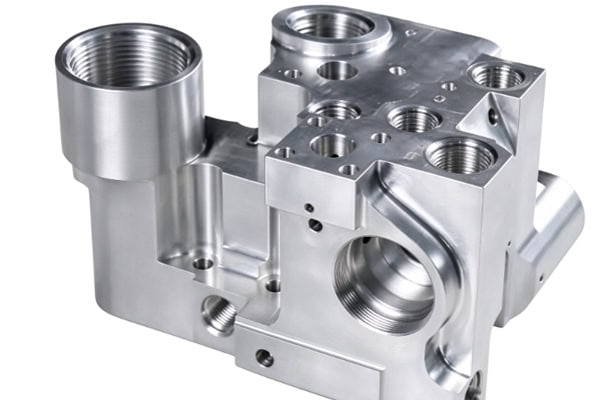
Instrument Housings and Mounting Structural Parts
These components mainly provide equipment protection, module mounting, and structural connection, making weight and assembly dimensions important considerations.
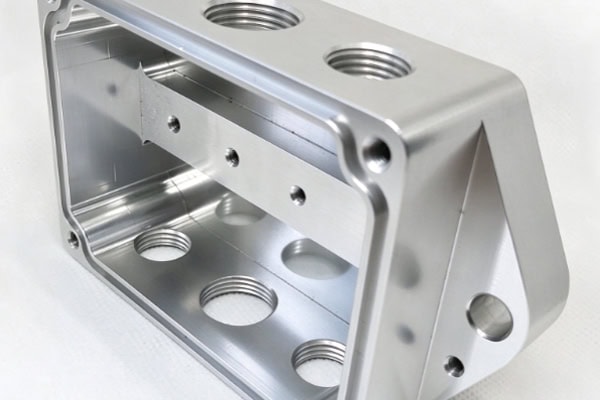
- Instrument Housings: Can be machined with mounting holes, internal cavities, connection slots, and sensor interfaces.
- Mounting Panels: Suitable for equipment panels, module mounting plates, and structural parts around operating areas.
- Support Brackets and Connectors: CNC milling can produce positioning holes, connection holes, and weight-reduction structures.
Proper structural design can balance equipment weight with ease of subsequent assembly.
Auxiliary Instrument and Non-Pressure-Bearing Structural Parts
Some inspection, monitoring, and auxiliary equipment requires both portability and structural stability, allowing aluminum alloy solutions to be considered after application-specific verification.
- Suitable for certain sensor brackets, protective covers, and instrument mounting bases.
- Multi-axis machining can handle side holes, angled surfaces, and complex contours.
- Precision locating surfaces help maintain the installation relationships between instrument modules.
Parts used as pressure boundaries, critical load-bearing components, or components exposed to severe downhole conditions require separate material and structural verification.
How Can the Machining Quality of Aluminum Alloy Parts for Oil & Gas Equipment Be Controlled?
The final quality of aluminum alloy parts depends on material condition, structural design, fixturing, and cutting processes.
Select the Material Grade According to Actual Operating Conditions
Different aluminum alloys vary in strength, corrosion resistance, heat-treatment condition, and machinability, so material selection should not be based solely on strength.
| Delkrav | Materialer at overveje | Bearbejdningsfokus | Hovedprogrammet |
| General non-pressure-bearing structures | 6061-T6 and similar grades | Dimensions, flatness | Mounting plates, brackets |
| Structures with higher corrosion-resistance requirements | 5xxx or suitable 6xxx series | Miljøkompatibilitet | Certain external structures |
| Instrument structural parts | 6061 series and similar grades | Hole positions, datums, surface quality | Housings, mounting bases |
| Special lightweight components | Determined through design verification | Strength, corrosion, stress condition | Specific structural components |
Although 7075 offers high strength, its corrosion resistance and susceptibility to stress corrosion cracking require careful evaluation in oil and gas environments. It should not be treated as a routine recommendation for high-load structural parts in corrosive service. The specific grade should be determined according to temperature, media, loads, and applicable design requirements.
Control Machining Deformation of Aluminum Alloy Parts
Large mounting plates, thin-wall housings, and parts requiring substantial material removal can be affected by residual stress and fixturing methods, so the machining sequence should be planned in advance.
- Leave Appropriate Machining Allowance: Avoid removing excessive material during rough machining.
- Use Staged Machining: Arrange rough and finish machining according to the part structure.
- Control Clamping Force: Reduce localized deformation caused by excessive clamping on thin-wall areas.
- Optimize Cutting Parameters: Minimize the effects of vibration, burrs, and machining heat on dimensions.
A well-planned machining sequence helps improve dimensional stability in complex aluminum alloy parts.
Arrange Quality Inspection According to Critical Features
Inspection methods should be determined according to drawing tolerances and actual assembly functions rather than applying the same method to every dimension.Mounting holes, locating surfaces, connection holes, and precision-fit areas can be inspected using calipers, micrometers, height gauges, vision measuring systems, or coordinate measuring machines according to the specified tolerances. During batch production, material condition, machining programs, and inspection standards for critical dimensions should also remain consistent. Establishing inspection procedures around critical features helps reduce dimensional issues during assembly.
How Should Corrosion Protection and Surface Requirements Be Addressed for Aluminum Alloy Parts?
Oil and gas equipment may operate in environments involving moisture, salt, chloride ions, or specific chemical media. Surface treatment therefore needs to be selected according to actual service conditions.
Bestem overfladebehandling i henhold til driftsmiljøet
Surface treatment should be planned with corrosion resistance, wear resistance, dimensional changes, and assembly relationships considered together.
- Anodizing: Suitable for certain non-pressure-bearing structural parts requiring improved surface corrosion and wear resistance.
- Hard Anodizing: Can be considered for areas subject to friction or higher wear requirements.
- Local Masking: Precision holes, threads, and special contact areas should have their treatment boundaries planned in advance.
For precision-fit areas, dimensional changes caused by the treatment layer should be included when determining machining allowances.
Define the Application Boundaries of Aluminum Alloy
Aluminum alloy used in oil and gas equipment cannot simply be treated like ordinary industrial structural material. Its application range must be determined according to design conditions and applicable requirements. Ordinary aluminum alloy parts should not be used for pressure boundaries, wellhead pressure-control equipment, or critical high-load components without engineering verification. The oil and gas industry does have specially designed dissolvable aluminum alloy downhole tools, whose material properties and operating conditions are specifically verified. Conventional CNC aluminum alloy projects should primarily focus on non-pressure-bearing housings, panels, brackets, and mounting bases.
Perform Proper Cleaning and Protection After Machining
After cutting is completed, burrs, residues, and potential surface damage during transportation also need to be addressed.
- Perform deburring, cleaning, and surface inspection according to project requirements.
- Provide appropriate packaging protection for parts that have undergone anodizing or other surface treatments.
- Check treatment-layer integrity and final dimensions in precision-fit areas.
Proper post-processing helps parts proceed smoothly into subsequent assembly operations.
What Capabilities Should an Oil & Gas Equipment Aluminum Alloy CNC Supplier Have?
For purchasers, machining equipment is only one part of a supplier’s capabilities. Material management, quality documentation, and project response also affect delivery results.
Ability to Machine Complex Aluminum Alloy Structures
Suppliers need to develop targeted manufacturing processes according to part dimensions, wall thickness, and machining features.
- Support machining of deep cavities, thin walls, multiple holes, and multi-sided structures.
- Adjust tooling, spindle speed, feed rate, and cooling methods according to aluminum alloy characteristics.
- Support prototype, small-batch, and repeat-order production.
Proper process configuration can reduce trial machining and rework while improving order execution stability.
Complete Quality and Project Coordination Capabilities
Oil and gas equipment procurement often involves material certificates, dimensional inspection, surface treatment, and delivery documentation. Suppliers should be able to establish appropriate production records based on project requirements and promptly update machining processes when drawings are revised. For special projects, material grade, heat-treatment condition, critical dimensions, surface treatment, and acceptance requirements should also be confirmed before production. Clear project management helps engineering, procurement, and manufacturing teams maintain smooth coordination.
The key to manufacturing aluminum alloy parts for oil and gas equipment is to match material properties, part functions, and field conditions. When defining the manufacturing plan, procurement and engineering teams should verify the material grade, drawing tolerances, surface treatment, inspection documentation, and batch delivery requirements, while special-service components should undergo engineering verification before production. TiRapid provides CNC precision machining services for custom aluminum alloy parts used in oil and gas equipment, supporting prototype development and small-batch production.
















